
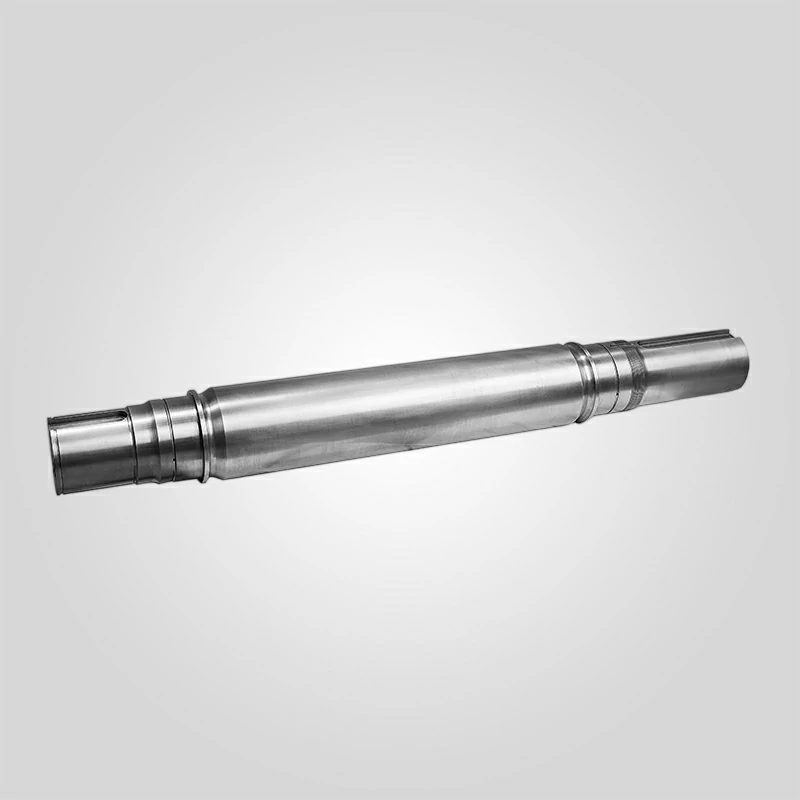
Flsmidth Cone Crusher Pinion Shaft
Part Type: Pinion Shaft Assembly
Compatibility: Flsmidth KB Series cone crushers
Material: High-strength alloy steel forging
Surface Hardness: 58-62 HRC
PRODUCT
Description
FLSmidth Cone Crusher Pinion Shaft: Precision Power Transmission
The Pinion Shaft (Countershaft) is the primary input drive component for FLSmidth cone crushers, including the Raptor XL Series and legacy KB models. It transmits rotational torque from the motor sheave to the eccentric assembly via a high-precision Spiral Bevel Gear set. Unlike static Wear parts, this is a dynamic, high-load component that demands zero-defect metallurgy.
As specialized crusher part suppliers, we manufacture these shafts using vacuum-degassed forged steel. Our gears are Gleason-ground to ensure optimal contact patterns (40-50% load bearing), reducing noise and extending the service life of the entire drive train.
Technical Specifications & Metallurgy
We adhere to strict AGMA/DIN gear standards. The following specifications apply to our FLSmidth compatible pinion shafts.
| Technical Parameter | Specification Details |
|---|---|
| Compatible Equipment | FLSmidth Raptor XL300, XL400, XL500, XL900 |
| Shaft Material | Forged 18CrNiMo7-6 (DIN 1.6587) or 17CrNiMo6 |
| Gear Type | Spiral Bevel Gear (Gleason Profile) |
| Heat Treatment | Carburizing (Case Hardening) + Quenching |
| Surface Hardness | 58 – 62 HRC (Case Depth 1.8 – 2.5mm) |
| Core Toughness | 32 – 38 HRC (Impact Resistant Core) |
| Machining Precision | Gear: DIN Grade 6 | Shaft: ISO k6/m6 |
| Service Life | 12,000 – 18,000 Hours (Clean Oil Condition) |
| Weight Range | 150 – 450 kg (Varies by Model) |
Performance Engineering: The Raptor Standard
FLSmidth Raptor crushers are known for high power density. Our Pinion Shafts are engineered to match this:
- Forged Integrity: We use Open Die Forging with a reduction ratio > 3:1. This aligns the grain flow along the shaft axis, increasing torsional fatigue strength by 40% compared to rolled bar stock.
- Precision Grinding: The bearing journals are ground to Ra 0.8μm tolerances to ensure a perfect fit with the pinion shaft bearings (Cartridge bushings). This prevents the “shaft wobble” that destroys oil seals.
- Shot Peening: The gear roots are shot peened to induce compressive residual stress, preventing fatigue cracks at the base of the teeth.
Field Diagnosis: “Vibration Signatures”
Catch failures before they happen.
The Symptom: Monitor vibration. If you see a spike at the Gear Mesh Frequency (GMF) (Shaft Speed x Number of Teeth), it usually means gear wear or misalignment.
The Symptom: If you see a spike at 1x Shaft Running Speed, it usually means the pinion shaft is bent or the assembly is out of balance.
The Action: Check the backlash immediately. Also, inspect the magnetic plugs for “chunky” steel particles, which indicate gear spalling.
Supply Chain & Installation
We supply complete Pinion Shaft Assemblies (shaft + gear + bearings + housing) or individual shafts. Replacing the entire cartridge is often faster (2 hours) than rebuilding a shaft (8+ hours) on site.
Expert Engineer’s Note: Oil Seals
Critical Tip: The FLSmidth pinion shaft uses a labyrinth or lip seal. When replacing the shaft, always replace the seal carrier o-rings and the main oil seal. A $50 seal failure will let dust into the housing, destroying a $5,000 shaft in days. Ensure the seal journal on the shaft is polished and free of nicks.
“Authoritative Engineering Data: All critical metallurgical specifications and dimensional tolerances (e.g., ±0.05mm) are strictly governed by the master English documentation. While localized versions are provided for operational reference, the English original remains the sole binding authority for quality inspection and technical compliance.”





 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish