

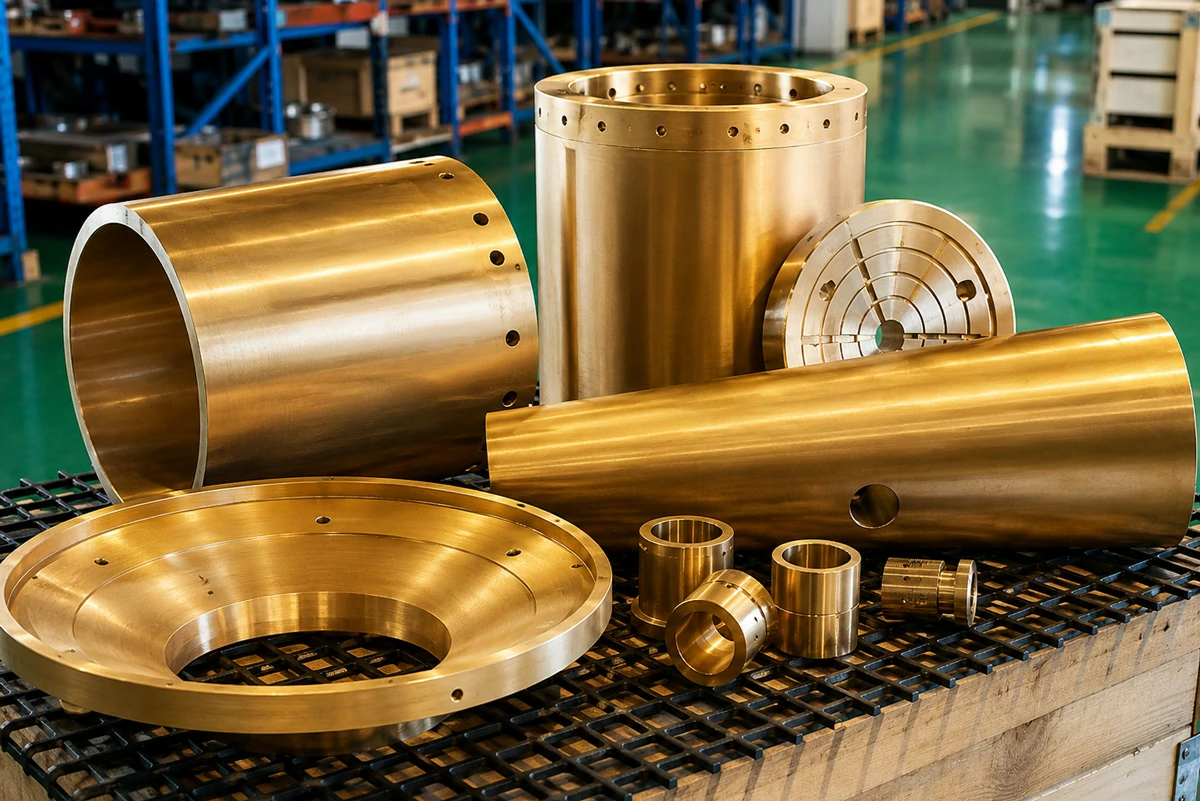
Factory Material Composition Testing Is the First Wear-Life Test for Crusher Parts
A jaw plate can look perfect after shot blasting and still lose 30 percent of its expected life if the manganese, carbon, chromium, or molybdenum content is outside the required range. A cone liner can pass a visual inspection and still crack early if the alloy is too brittle for the feed impact. An impact crusher blow bar can show high hardness on paper and still fail in service if the chemistry creates the wrong carbide structure. That is why factory material composition testing is not a paperwork formality. It is the first real test of crusher parts material quality before the part ever reaches a quarry or mine site.
Crusher parts work in a severe combination of impact, compression, sliding abrasion, gouging wear, heat, dust, and vibration. The main wear parts include jaw plates, cone crusher mantles, concaves, cheek plates, impact crusher blow bars, hammer heads, liners, side plates, roll crusher segments, and VSI wear tips. Each part faces a different balance of impact and abrasion. Because of that, one material cannot solve every wear problem. Good crusher parts material selection depends on feed size, rock abrasiveness, moisture, tramp metal risk, crusher speed, chamber design, and maintenance practice.
In the workshop and in the field, I have seen many early failures that were not caused by poor operation alone. Some failures began in the melt. If the chemical composition was wrong, heat treatment could not fully rescue the casting. If the carbon level was too high in the wrong steel, toughness dropped. If manganese was too low in high manganese steel, work hardening became weak. If chromium was too high for a high-impact application, the part became wear resistant but too brittle. A good material ratio is not only a chemical number. It is the foundation of service life.
Why Chemical Composition Must Be Tested Before Shipment
Factory material composition testing confirms that the casting matches the purchase order, drawing, standard, and operating condition. For crusher wear parts, the difference between a correct alloy and a wrong alloy is often invisible to the eye. Two blow bars may have the same shape and weight, but one may be martensitic steel, one may be high chromium white iron, and one may be high manganese steel. Their field behavior will be completely different.
A reliable factory should test material composition at more than one stage. The first check is normally made during melting, before pouring, so the foundry can adjust alloy elements while the metal is still liquid. The second check should be made from a test block, casting coupon, or representative sample after casting. For critical crusher parts, final positive material identification can be used before shipment to reduce the risk of mix-ups between different grades.
The most common methods include optical emission spectrometry, chemical laboratory analysis, and positive material identification. Optical emission spectrometry is widely used in foundries because it can analyze many metallic elements quickly and accurately. For steel grades where carbon, phosphorus, and sulfur are important, the testing method must be selected carefully because handheld XRF is useful for many alloy elements but is not enough for every light element requirement. The inspection report should show the method, sample source, heat number, specification range, measured result, and pass or fail judgment.
Common Crusher Parts Material Choices and Their Working Logic
High manganese steel is widely used for jaw plates, cone crusher liners, mantles, concaves, and some hammer applications. The classic Hadfield-type manganese steel is known for high toughness and work hardening behavior. A common ASTM A128 Grade A type composition may contain about 1.05 to 1.35 percent carbon, around 11 percent manganese, about 1 percent silicon, and iron as the balance. In service, high manganese steel can start near a moderate Brinell hardness and work harden under heavy impact, with surface hardness often rising significantly when the crushing pressure is high enough.
This is why manganese steel performs well in primary crushing with large feed and strong impact. The surface becomes harder as rock repeatedly compresses and strikes the liner. At the same time, the inner core remains tough enough to resist cracking. But the material must have the right chemistry. If the manganese-to-carbon balance is poor, the liner may not harden properly or may become brittle. If phosphorus or sulfur is too high, cracking risk increases. If heat treatment is not controlled, carbides may remain at grain boundaries and reduce toughness.
High chromium white iron is often selected for impact crusher blow bars, secondary crushing liners, and applications with clean, abrasive material and limited tramp iron. ASTM A532 covers abrasion-resistant white cast irons used in mining, milling, earth-handling, and manufacturing industries. A typical Class III Type A 25 percent chromium white iron range may include about 2.0 to 3.3 percent carbon and 23.0 to 30.0 percent chromium, with controlled limits for manganese, silicon, nickel, molybdenum, copper, phosphorus, and sulfur. Its wear resistance comes from hard chromium carbides and a hard matrix.
High chromium material can give excellent service life in abrasive stone, but it is not suitable for every crusher. If uncrushable steel enters the chamber, a high chrome blow bar may crack or break because its toughness is lower than manganese steel or martensitic steel. This is why material testing must be connected with application review. A correct chemical composition for one machine may be the wrong material choice for another machine.
Martensitic alloy steel is often used where the application requires a balance between impact toughness and wear resistance. It does not usually match high chrome iron in pure abrasion resistance, but it can tolerate impact better. Some martensitic crusher parts include chromium and molybdenum to improve hardenability, strength, and wear resistance. The final performance depends not only on composition but also on heat treatment, section thickness, quenching practice, and tempering control.
How Material Ratio Changes Wear Life
Carbon is one of the most important elements in steel and cast iron wear parts. In high manganese steel, carbon supports strength and work hardening, but excessive carbon or poor heat treatment can make the casting brittle. In high chromium white iron, carbon combines with chromium to form hard carbides. Too little carbon may reduce abrasion resistance, while too much carbon can increase brittleness and make machining or impact service more difficult.
Manganese stabilizes the austenitic structure in high manganese steel and supports toughness. In jaw plates and cone liners, this is critical because the part must absorb repeated impact without cracking. A manganese steel liner with weak chemistry may wear fast because it does not work harden enough. On the other hand, simply increasing manganese without understanding carbon, section size, and heat treatment does not automatically create a better liner.
Chromium improves wear resistance by promoting hard carbides in white iron and by supporting hardenability in alloy steel. In high chrome blow bars, chromium is a main wear-life element. But chromium also changes toughness. A high chromium part should be used where abrasion is severe and impact is controlled. It should not be selected only because the hardness number looks attractive.
Molybdenum, nickel, and copper may be added to improve hardenability, toughness, or matrix structure depending on the alloy system. Silicon helps deoxidation and can influence casting behavior, but excessive silicon may affect mechanical properties. Phosphorus and sulfur are usually controlled as harmful residual elements because they can reduce toughness and increase crack sensitivity. These small percentages matter. In a crusher, a tiny chemistry deviation can become a large downtime problem.
What a Proper Factory Material Test Report Should Include
A useful material report for crusher parts should be traceable and specific. It should not only say “material qualified.” It should list the heat number, part number, casting batch, sample location, material grade, standard or customer specification, chemical composition range, actual measured value, hardness result, heat treatment condition, inspection date, and inspector approval. For critical wear parts, the report should also match the marking on the casting.
| Inspection item | Why it matters | Typical evidence required |
|---|---|---|
| Chemical composition | Confirms that the crusher parts material matches the ordered alloy grade and expected wear mechanism. | Spectrometer report, laboratory report, heat number, measured element values, and specification limits. |
| Hardness | Shows whether heat treatment and matrix condition are suitable for the application. | HB, HRC, or HV test result according to the drawing or purchase requirement. |
| Heat treatment record | Confirms that the casting received the correct quenching, tempering, stress relief, or solution treatment. | Furnace chart, temperature record, holding time, cooling method, and batch traceability. |
| Traceability marking | Prevents mixed grades from being shipped to the customer. | Cast or stamped heat number, part code, material grade, and inspection tag. |
| Visual and dimensional inspection | Ensures that the correct material is also supplied in the correct shape and fit condition. | Dimension report, surface inspection record, and packing verification. |
Field Failure Review: The Cost of Skipping Composition Verification
I once handled a failure case on a secondary impact crusher where a set of blow bars wore unevenly and one bar cracked before reaching half of the expected working hours. The customer first suspected wrong rotor speed and poor feed control. After checking the machine, the feed size, and the wear pattern, I asked for the original material report. The document only showed hardness, not chemical composition. The supplier had shipped the parts as high chrome, but later sample testing showed the chromium content was below the required range for the ordered grade, and the carbon balance was also inconsistent.
From a distance, the blow bar looked acceptable. The surface hardness reading was not alarming. But the microstructure did not have the right carbide support for the abrasive stone. The part wore fast at the impact zone, then stress concentrated near the worn edge. Once the crack started, the rotor load became unbalanced and vibration increased. The final loss was not just one set of blow bars. The site lost production time, labor, emergency freight, and confidence in the supply chain.
That case is the reason I tell buyers to treat material testing as a production safeguard, not an optional certificate. A low price without chemistry verification is not a saving. It is a hidden risk transferred to the crusher.
Why Hardness Alone Cannot Prove Material Quality
Many purchasing teams ask only for hardness because it is easy to understand. Hardness is important, but it cannot replace chemical analysis. A high chromium iron part and a martensitic steel part may show similar hardness ranges, yet their toughness and wear behavior can be very different. A high manganese steel liner may not have extremely high initial hardness, but it can work harden under proper impact conditions. If a buyer rejects it only because the first hardness value is lower than a high chrome part, the material selection logic is wrong.
Hardness tells part of the story. Chemical composition tells whether the alloy has the right building blocks. Heat treatment tells whether the structure was developed correctly. Field performance tells whether the selected material matches the crushing condition. Good crusher parts material control must connect all four.
How Buyers Should Specify Material Requirements
To avoid disputes, the purchase order should define the material grade, applicable standard, expected chemical composition range, hardness range, heat treatment condition, testing method, and report format. For example, a jaw plate order should not simply say “manganese steel.” It should identify whether the requirement is Mn13, Mn18, Mn22, or another grade, and whether chromium, molybdenum, or other alloy additions are required. A blow bar order should clearly state whether the application needs high chrome white iron, martensitic steel, ceramic insert material, or manganese steel.
The buyer should also tell the foundry the real working condition. Feed material, compressive strength, silica content, moisture, feed size, tramp iron risk, and crusher model all affect material selection. A supplier cannot choose the best material ratio if the operating condition is hidden. The more accurate the application information, the easier it is to choose a material that balances wear resistance and toughness.
Final View: Material Composition Is the DNA of Crusher Parts
Crusher parts do not fail randomly. Most failures can be traced to one or more causes: wrong material, unstable chemistry, poor heat treatment, casting defects, incorrect fit, unsuitable operation, or poor maintenance. Among these causes, material composition is the earliest point of control. Once the wrong chemistry has been poured, every later process is limited by that mistake.
Factory material composition testing protects the buyer, the foundry, and the mine site. It proves that the crusher parts material matches the required grade. It helps predict wear behavior before the part enters service. It prevents mixed materials from reaching the customer. It supports traceability when a failure investigation is needed. Most importantly, it connects the chemical design of the casting with the real working life of the crusher.
A good material ratio gives crusher parts the ability to resist impact, develop work hardening, form stable carbides, maintain toughness, and survive abrasive contact. A poor material ratio may save a small amount in alloy cost, but it can shorten service life, increase downtime, damage shafts or rotors, and raise the total cost per ton. For any serious quarry, cement plant, recycling operation, or mine, the question should not be whether factory material testing is necessary. The real question is whether the test report is detailed enough to prove that the part is ready for the crushing chamber.


 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish