

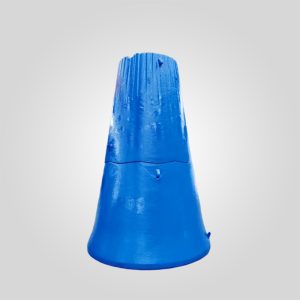
KB63-89 Bronze Protective Cap 4470332 | Gyratory Crusher Spares
Material:ZCuPb20Sn5, ZCuPb10Sn10 ZCuPb24Sn5
Model:KB63-89, KB54-75 , BK54-75, KB54-67, KB63-75
Weights(kg): 171kgs Item code: 4470332,2080688674
Our company undertakes the customized bronze parts of crushers.
库存 182 件
PRODUCT
Description
Technical Specifications: KB Series Bronze Protective Cap
The Bronze Protective Cap (Item Codes: 4470332 / 2080688674) is a critical sealing and wear component within the Thyssenkrupp gyratory crusher assembly. Unlike structural steel caps, this component utilizes high-leaded bronze to provide a self-lubricating barrier, often functioning within the dust seal or eccentric protection assembly. Below are the engineering specifications.
| Technical Parameter | Specification Data |
|---|---|
| OEM Item Codes | 4470332, 2080688674 |
| Material Grade | ZCuPb20Sn5 (High Leaded Tin Bronze) |
| Manufacturing Process | Centrifugal Casting (High G-Force Densification) |
| Net Weight | 171 kg (±1.5% Tolerance) |
| Hardness | 70 – 80 HBW (Optimized for conformity) |
| Tensile Strength | ≥ 200 MPa |
| Machining Precision | ISO 2768-mK / Surface Finish Ra 1.6μm |
| Compatible Models | KB63-89, KB54-75, BK54-75, KB54-67, KB63-75 |
Core Advantages: Metallurgy and Manufacturing
In the harsh environment of primary crushing, contamination is the enemy of longevity. This protective cap is engineered not just as a physical barrier, but as a tribological safeguard. We utilize ZCuPb20Sn5, a specialized bronze alloy containing 20% Lead (Pb) and 5% Tin (Sn).
Why Centrifugal Casting Matters
For a 171kg bronze component, internal integrity is non-negotiable. Standard sand casting often results in “lead segregation,” where the lead pools at the bottom of the mold, creating weak spots. We employ Centrifugal Casting technology for these crusher spares. By spinning the mold at high velocities during solidification, we achieve:
- Uniform Lead Dispersion: The lead exists as microscopic globules evenly distributed throughout the copper matrix, ensuring consistent self-lubrication across the entire wear surface.
- Higher Density: Impurities and gas pockets are forced to the bore (which is machined away), leaving a dense, defect-free crystal structure.
- Enhanced Wear Life: The dense structure resists the abrasive action of dust ingress better than porous sand-cast alternatives.
Performance Comparison
Replacing OEM parts requires confidence in performance. Our centrifugal bronze caps offer distinct advantages over standard market replacements.
| Performance Metric | Standard Sand-Cast Bronze | Our Centrifugal ZCuPb20Sn5 Cap |
|---|---|---|
| Microstructure | Coarse grain, potential porosity | Fine grain, 100% dense |
| Friction Coefficient | 0.08 – 0.12 (Mixed) | 0.05 – 0.08 (Superior Lubricity) |
| Impact Resistance | Low (Brittle) | Moderate (Improved Ductility) |
| Maintenance Interval | Standard Cycle | Extended by 20-30% |
Field Diagnostic & Maintenance Tips
As a specialized crusher part supplier, we advise paying close attention to this component during liner changes. It is often overlooked until a seal failure occurs.
1. Visual Scoring Check: Inspect the running surface of the cap. Deep circumferential scoring indicates the ingress of coarse abrasive particles (tramp material). If grooves exceed 1mm in depth, the self-lubricating film is compromised, and the cap must be replaced to prevent damage to the mating steel.
2. Profile Deformation: Use a profile gauge to check the geometry. Because ZCuPb20Sn5 is a relatively soft bronze (approx. 75 HB), it can deform under uneven pressure. Significant deformation indicates an alignment issue in the dust seal assembly.
Quality Assurance
Every batch of our bronze castings undergoes rigorous testing before dispatch:
- Spectral Analysis: Verifies the Copper, Lead, and Tin ratios meet DIN/ASTM standards.
- Dimensional Inspection: CMM measurement ensures the mounting fit is within H7/h6 tolerance zones.
- PT Testing: Dye penetrant inspection on machined surfaces to ensure no surface porosity exists.
When installing this bronze protective cap (4470332), ensure the mating steel surface is polished and free of burrs. Even a small burr on the steel side can act as a cutting tool against the soft leaded bronze, destroying the part within the first 100 hours of operation. We recommend applying a light coat of Moly-paste during assembly to protect the bronze during the initial break-in period.
Expert Note on Supply
From the Engineer’s Desk: The Protective Cap is a vital part of the crusher’s defense system. Using a sub-standard bronze alloy with low lead content reduces cost but significantly increases the risk of friction welding or seal failure. Our ZCuPb20Sn5 alloy is formulated specifically to handle the low-speed, high-load conditions of large primary gyratories.
As a manufacturer of crusher parts, we specialize in heavy-duty bronze components. We provide full traceability and material certificates with every shipment, ensuring you receive OEM-equivalent quality for your Thyssenkrupp fleet.
“Authoritative Engineering Data: All critical metallurgical specifications and dimensional tolerances (e.g., ±0.05mm) are strictly governed by the master English documentation. While localized versions are provided for operational reference, the English original remains the sole binding authority for quality inspection and technical compliance.”


 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish