
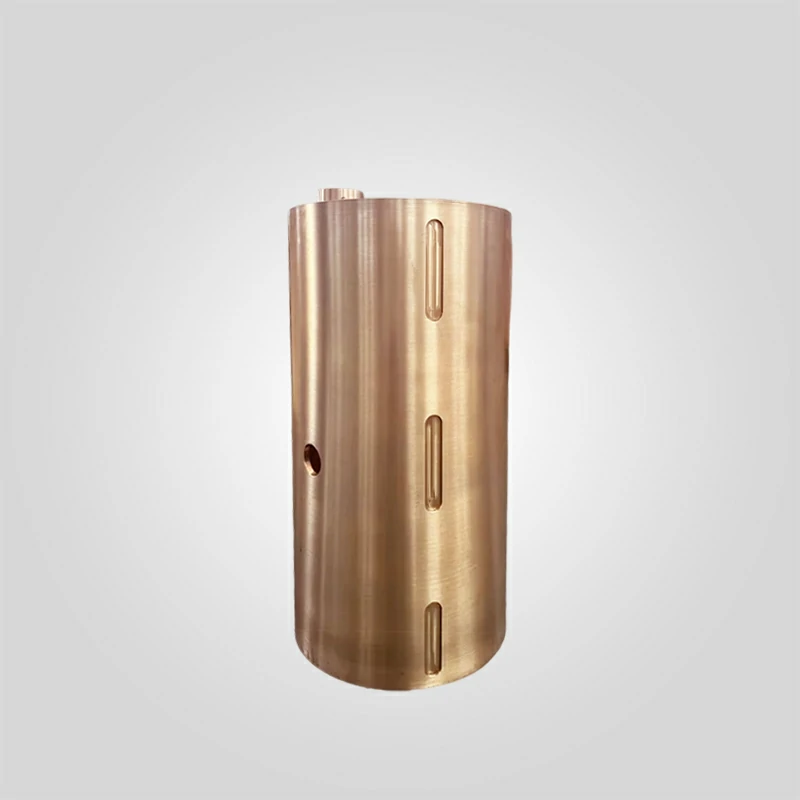
Outer Eccentric Bushing 2214-5321 | Symons 4¼ Ft Cone Crusher | C93700 Bronze
Material : SAE 660 Bronze Alloy (CuSn5Pb5)
Hardness :HB 60-70
Temperature Resistance: Up to 200°C (392°F)
Pressure Capacity :≥50 MPa
Compatibility :Symons 2ft, 3ft, 4ft, 5.5ft, 7ft series
库存 121 件
PRODUCT
Description
The Outer Eccentric Bushing (Part Number: 2214-5321) is the stationary bearing element housed within the Main Frame of the Symons 4 ¼ Ft Cone Crusher. It supports the rotating Eccentric Assembly.
Unlike standard SAE 660 bushings offered by generic crusher part suppliers, our components are manufactured using Centrifugal Casting technology from SAE 64 (UNS C93700) High-Lead Tin Bronze. This premium metallurgy ensures superior “anti-friction” properties, preventing catastrophic seizure (burning) even during momentary lubrication lapses or tramp iron overload events.
Technical Specifications
| Technical Parameter | Specification Value | Engineering Standard |
|---|---|---|
| OEM Part Number | 2214-5321 | Symons 4 ¼ Ft (Standard / Short Head) |
| Material Grade | C93700 High-Lead Tin Bronze (SAE 64) | Superior to SAE 660 for heavy loads |
| Manufacturing Process | Centrifugal Casting (Spun Cast) | Eliminates porosity & gas pockets |
| Chemical Composition | Cu: 80%, Sn: 10%, Pb: 10% | High Lead content for self-lubrication |
| Hardness | 60 – 70 HBW | Optimized for embeddability of debris |
| Tensile Strength | ≥ 240 MPa | ASTM B271 Standard |
| Machining Tolerance | Outer Dia: p6 / Inner Dia: E7 | Interference fit with Main Frame |
| Weight | ~ 77.7 kg | Solid Machined Weight |
Performance & Diagnostics: Preventing Frame Damage
The Outer Bronze Bushing is a “Sacrificial Part.” Its job is to wear out so that your expensive Main Frame does not.
- Centrifugal vs. Sand Cast: Our centrifugally cast bushings have a dense, fine-grained structure. This increases compressive strength by 15% compared to sand-cast alternatives, reducing the risk of the bushing cracking under the “crushing stroke.”
- Thermal Conductivity: High-grade C93700 bronze dissipates heat rapidly. If the bushing runs too hot (>60°C return oil temp), the oil film breaks down. Our material quality helps maintain the hydrodynamic wedge.
Engineer’s Maintenance Advice (Information Gain)
Diagnostic: The “Main Frame Bore” Check
Before installing a new 2214-5321 bushing, you MUST inspect the Main Frame bore.
- The Risk: If the old bushing spun in the frame, the frame bore may be worn or oval.
- The Limit: Measure the frame bore at the top, middle, and bottom. If the ovality exceeds 0.05mm, the new bushing will not have full contact. This creates “hot spots” and leads to premature failure (often within 200 hours).
- Installation Tip: This is a “Freeze Fit” component. Use Dry Ice (Solid CO2) to shrink the bushing for at least 2 hours before dropping it into the frame. Do NOT use a sledgehammer, as this distorts the soft bronze.
Quality Assurance
We supply reliable crusher spares that keep your plant running. Every bronze bushing includes:
- Material Certificate: Proving Lead/Tin content (Spectrometer Analysis).
- Dimensional Report: Verifying the OD interference fit tolerance.
- DPI Test: Dye Penetrant Inspection to ensure no surface cracks.
Need to confirm the fit for your Symons 4.25′? Contact our engineering team.
“Authoritative Engineering Data: All critical metallurgical specifications and dimensional tolerances (e.g., ±0.05mm) are strictly governed by the master English documentation. While localized versions are provided for operational reference, the English original remains the sole binding authority for quality inspection and technical compliance.”






 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish