
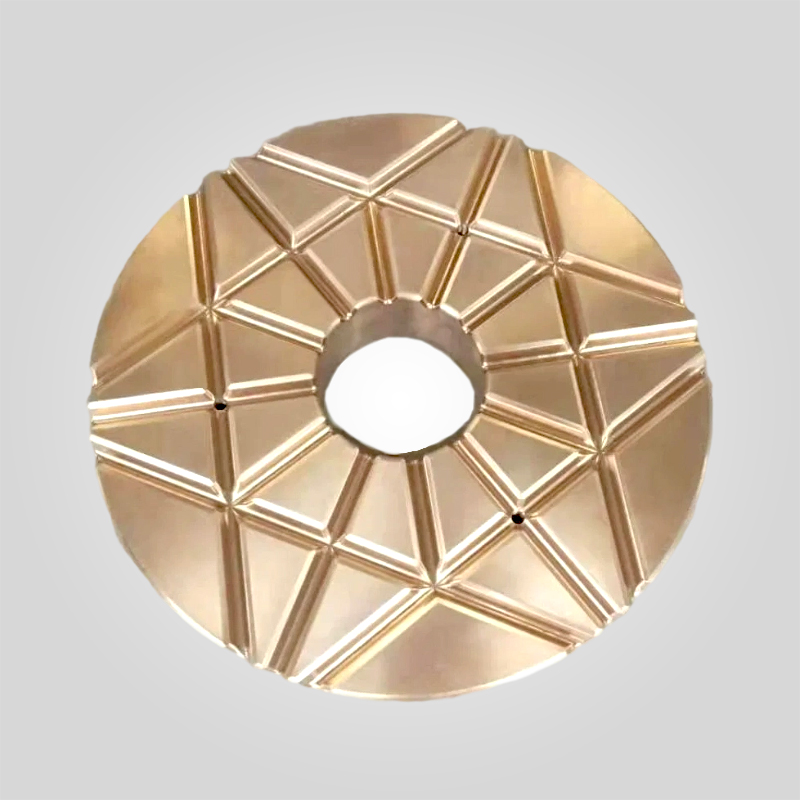
Sandvik CH440 Piston Wearing Plate | 442.8730-01 Step Washer
Model NO.: CH660 CONE CRUSHER
Certification: CE, RoHS, ISO 9001:2000, ISO 9001:2008
Standard: AISI, ASME, BS, ANSI, JIS, GB, GOST, ASTM, DIN
Surface Treatment: Polishing
Manufacturing Process: Casting
Material: Copper Alloy
Transport Package: Crated
Specification: Bronze
库存 182 件
PRODUCT
Description
Technical Specifications: Sandvik CH440 Piston Wearing Plate
| Specification Attribute | Engineering Standard |
|---|---|
| Part Name | Piston Wearing Plate (Step Washer) |
| OEM Part Number | 442.8730-01 |
| Reference Code | R 223.1117, 11 |
| Compatible Equipment | Sandvik CH440 / S4800 Hydrocone |
| Material Grade | High-Leaded Tin Bronze (ASTM B505 C93700 / SAE 64) |
| Net Weight | 38.85 kg |
| Surface Finish | Ra 0.4 (Lapped Finish) |
| Flatness Tolerance | ≤ 0.02mm (Critical for oil film) |
The Piston Wearing Plate (442.8730-01) is the critical axial bearing at the heart of the Sandvik CH440 Hydroset system.
As specialized crusher part suppliers, we understand that this single component supports the entire weight of the moving assembly (Mainshaft + Mantle) plus the dynamic crushing force.
Our replacements are engineered from premium Leaded Bronze to prevent catastrophic seizing of the Hydroset cylinder.
Core Advantages: Metallurgy & Precision Lapping
The failure of a Step Washer usually means the destruction of the Mainshaft.
Our Spare parts manufacturing process prioritizes tribology (friction science):
- High-Leaded Bronze (C93700): We utilize an alloy with 20-22% Lead content.
Under extreme axial loads, the lead creates a microscopic self-lubricating film.
This provides a “fail-safe” mechanism during startup or shut-down when hydrostatic oil pressure is low. - Centrifugal Casting: Gravity casting cannot achieve the density required for a 38kg thrust bearing.
Our plates are centrifugally cast to eliminate porosity, ensuring the plate can withstand compressive loads exceeding 150 MPa without deforming. - Precision Lapping: After CNC machining, every plate undergoes a flat lapping process.
This achieves a flatness tolerance of <0.02mm, which is essential for maintaining the high-pressure oil wedge that separates the plate from the steel piston.
Performance Comparison: Why Flatness Matters
In a Hydrocone crusher, the “Wearing Plate” must float on oil.
See why our precision Crusher spares outperform standard cast parts:
| Feature | Standard Turned Plate | Our Lapped Plate (442.8730-01) |
|---|---|---|
| Surface Flatness | >0.05mm (Risk of contact) | ≤0.02mm (Perfect Oil Seal) |
| Material Density | Variable (Sand Cast) | High (Centrifugal Cast) |
| Oil Wedge Formation | Unstable | Stable (Reduced Friction) |
Field Diagnosis: Inspecting the Hydroset Bearing
When the mainshaft is removed, inspecting the 442.8730-01 plate is mandatory.
Look for these signs:
- Edge Loading (Polished on one side): If one side of the plate is mirror-polished and worn thin while the other is dull, the Mainshaft is bent
“Authoritative Engineering Data: All critical metallurgical specifications and dimensional tolerances (e.g., ±0.05mm) are strictly governed by the master English documentation. While localized versions are provided for operational reference, the English original remains the sole binding authority for quality inspection and technical compliance.”





 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish