

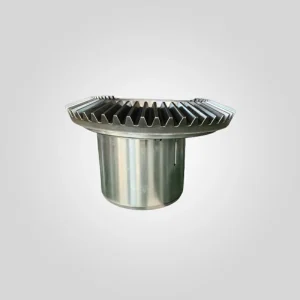
Cone Crusher Torch Ring | 6391-3321 Burning Ring | Sacrificial Spares
Superior Wear & Heat Resistance: Forged from Mn18Cr2 alloy steel (for extreme abrasion resistance) or CuSn8 tin bronze (for self-lubrication), this ring withstands hard feeds (granite, basalt) and high operating temperatures (≤200°C) without deformation. Outlasts generic steel rings by 30–50%.
Precision OEM Fit: Machined to exact original equipment tolerances, it installs seamlessly on Symons, Nordberg, and Terex cone crushers—no re-threading or adjustments needed. Eliminates misalignment-induced vibrations that damage spindles or bearings.
Cost-Effective Maintenance: Protects adjacent critical parts (e.g., spindles, eccentric bushings) from wear and debris—reducing spare parts replacement frequency by 25%+. Lowers your long-term maintenance budget.
Trusted Crusher Parts Suppliers Backing: As experienced crusher parts suppliers, we offer reverse-engineered OEM replicas and custom solutions for legacy crushers. Fast inventory and shipping to keep your operation running.
库存 72 件
PRODUCT
Description
Cone Crusher Torch Ring: Sacrificial Burning Ring | 6391-3321
The Torch Ring (Part No. 6391-3321), also known as the Burning Ring or Cutting Ring, is a critical sacrificial component for the liner retention system of Symons, Nordberg, and Sandvik cone crushers.
Installed between the Mantle (Moving Cone Liner) and the Head Nut (Locking Nut), this steel ring serves as a protective spacer.
Its primary engineering function is to facilitate the safe removal of worn liners. During operation, the crushing action self-tightens the Head Nut to immense torque levels; the Torch Ring is designed to be **flame-cut** during maintenance, instantly relieving this axial tension and allowing the nut to be spun off without damage to the spindle threads.
For mining maintenance teams sourcing from crusher part suppliers, the material composition of the Torch Ring is vital.
Our rings are manufactured from **Low Carbon Steel (ASTM A36 / S275)**.
Unlike generic “hard” rings, our alloy is selected specifically for its burn characteristics, ensuring a clean, fast cut that reduces liner changeout time by up to 30%.
Core Engineering Advantages
- Designed for Cutting: We use a normalized low-carbon steel grade that does not harden when heated. This prevents the torch cut from “wandering” and damaging the expensive Locking Nut or the Crusher Head seating surface.
- Head Nut Protection: By providing a 50mm sacrificial gap, the Torch Ring ensures the flame of the cutting torch is kept at a safe distance from the reusable Locking Nut and the Threaded Spindle.
- Compression Stability: Despite being cuttable, the ring has a yield strength sufficient to transmit the full clamping force of the locking assembly (up to 200 tons) to the mantle without mushrooming or creeping during operation.
Technical Specifications & Material Grade
Our Torch Rings are precision-machined to ensure flat, parallel faces for even load distribution on the mantle.
| Parameter | Specification | Standard/Notes |
|---|---|---|
| Part Number | 6391-3321 | OEM Interchangeable |
| Common Name | Torch Ring / Burning Ring | Sacrificial Cutting Washer |
| Material Grade | Low Carbon Steel | ASTM A36 / AISI 1020 / S235JR |
| Hardness | 120 – 150 HB | Soft for Oxy-Acetylene Cutting |
| Dimensions | OD: Φ250mm | ID: Φ180mm | H: 50mm | Corrected from Source |
| Net Weight | 5.25 kg | Solid Steel Ring |
| Surface Finish | Machined Faces (Ra 3.2) | Anti-Rust Oil Coated |
Compatible Crusher Models
The 6391-3321 Torch Ring is compatible with locking assemblies on various standard cone crushers:
| Brand Style | Crusher Size | Application |
|---|---|---|
| Symons / Gyradisc | 4.25ft, 5.5ft, 7ft | Standard & Short Head |
| Sandvik / Svedala | H-Series / S-Series | Mantle Locking Assembly |
| Nordberg / Metso | HP Series (Older Models) | Under Locking Nut |
Performance & Maintenance Efficiency
Using a proper Torch Ring is a safety and cost-saving measure:
- Prevents Spindle Damage: Without a Torch Ring, operators often try to hammer the nut loose or cut the nut itself. One slip with the torch can gouge the Main Shaft threads, ruining a component worth $50,000+. The $50 Torch Ring prevents this risk.
- Speed: A skilled welder can cut the Torch Ring in 5 minutes, causing the mantle to drop loose. This is significantly faster than trying to use a hydraulic nut runner on a seized nut.
Field Diagnosis: Installation Tips
Since this is a disposable part, inspection is about the **Locking Nut** and **Mantle**:
- New Installation: Always install a NEW Torch Ring with every liner change. Never try to reuse an old one, even if it wasn’t cut. It has been compressed and fatigued.
- Cutting Procedure: When cutting the ring, make two vertical cuts 180 degrees apart. Be careful not to cut into the Locking Nut above or the Mantle below (though the mantle is scrap anyway).
- Seating: Ensure the top of the Mantle and the bottom of the Locking Nut are clean. Debris under the Torch Ring will cause the nut to loosen during crushing.
Expert Engineer’s Note: Material Warning
Critical Maintenance Advice: Never manufacture a Torch Ring out of “spare scrap” high-tensile steel or Manganese.
If you use Manganese steel, you will likely be unable to cut it when the time comes, trapping the liner on the machine.
You will then have to wash the nut off with a carbon arc gouge, creating a massive amount of heat that can damage the head seals and bearings.
Always insist on Low Carbon Steel (Mild Steel) for Burning Rings.
“Authoritative Engineering Data: All critical metallurgical specifications and dimensional tolerances (e.g., ±0.05mm) are strictly governed by the master English documentation. While localized versions are provided for operational reference, the English original remains the sole binding authority for quality inspection and technical compliance.”




 English
 French
 German
 Spanish
 Russian
 Arabic
 Portuguese
 Turkish